How to Find a Reliable Beauty Device Manufacturer in 2026?

Time:2026-10-17 Author:Aria
0%

Choosing a dependable partner begins with a practical question: how to find a reliable beauty device manufacturer in 2026? The answer is not hidden in a glossy catalog. It appears in factory records, product testing, transparent communication, and consistent after-sales support. A trustworthy manufacturer should explain its quality system, provide traceable component records, and share relevant safety and performance documentation. Vague promises are warning signs.

Look closely.

W. Edwards Deming, a leading manufacturing quality expert, said, “Quality comes not from inspection, but from the improvement of the production process.” His principle remains highly relevant to beauty technology. Ask whether the supplier controls production before defects reach customers. Request a live factory video or an independent audit. Examine sample units for uneven seams, loose connectors, unclear labels, and inconsistent power output. Small details often reveal larger weaknesses.

Do not judge reliability from one successful sample. Review batch consistency, testing procedures, warranty terms, spare-parts availability, and response times for technical complaints. A serious manufacturer should discuss applicable quality and safety requirements without making unsupported certification claims. It should also explain how software, batteries, packaging, and user instructions are controlled. Even experienced buyers can miss hidden costs, especially custom tooling, minimum order quantities, and repeated testing. That deserves reflection. The lowest quotation may become the most expensive decision. This guide will show how to compare manufacturers carefully, verify their claims, and build a safer, more accountable supply relationship.

How to Find a Reliable Beauty Device Manufacturer in 2026?

Define the Device Class Using FDA 510(k) and EU MDR Requirements

How to Find a Reliable Beauty Device Manufacturer in 2026?

Finding a reliable beauty device manufacturer starts with regulatory classification, not factory photos. Define the intended use precisely: skin resurfacing, hair reduction, vascular treatment, or another claim. Then identify the energy source, contact time, invasiveness, and target users. These details shape the regulatory route. Under FDA rules, a device may need 510(k) clearance when it is substantially equivalent to a legally marketed predicate. Some devices are exempt, while higher-risk products may require another submission. A manufacturer promising “FDA approved” without naming the pathway deserves careful questioning. The wording matters.

For the EU market, apply EU MDR classification rules before discussing certificates. Risk class often depends on invasiveness, contact duration, active energy, and intended purpose. Classes I, IIa, IIb, and III involve increasing regulatory control. Special rules can change the result. A non-invasive appearance can mislead. Intense light or software functions may still create meaningful risk. Ask for a written classification rationale, not verbal assurance. Request the technical documentation index, clinical evaluation plan, risk-management file, and safety evidence.

During supplier audits, compare the approved design with the sample in your hand. Check labels, user instructions, calibration records, complaint handling, and change-control procedures. Confirm who owns the technical file and reports incidents after launch. A capable manufacturer should explain gaps openly and propose documented corrective action. It is not perfect evidence. Transparent uncertainty is safer than confident guessing. One overlooked claim can alter the device class, testing burden, and launch timeline. Let regulatory specialists review final claims before production begins.

Screen Suppliers Against ISO 13485 and McKinsey’s $590B 2028 Beauty Forecast

How to Find a Reliable Beauty Device Manufacturer in 2026?

McKinsey & Company forecasts the global beauty market could reach $590 billion by 2028. That growth attracts capable factories and opportunistic suppliers. Buyers should screen beyond glossy product photos and fast quotations. ISO 13485:2016 offers a stronger starting point because it emphasizes documented quality systems, risk management, traceability, and corrective actions.

During a supplier audit, request the quality manual, device history records, calibration logs, and recent CAPA reports. Check whether production staff can explain inspection steps without reading a script. A reliable manufacturer should also show controlled design changes, verified software, and batch-level material records. Ask how failed units are isolated. Watch the answer.

The supplier’s ISO certificate must match the actual facility and product scope. Verify its issuing body and expiration date independently. Certification alone is not proof of technical excellence. McKinsey’s beauty outlook also highlights consumer demand for science-backed, personalized devices, raising the need for credible testing and clear performance claims. Ask for test protocols, sample sizes, and raw results, not only polished summaries. Some suppliers may provide impressive documents but weak factory discipline. That gap deserves attention. A quiet production line is not necessarily a good one. Reference: McKinsey & Company, The State of Beauty 2023; ISO 13485:2016.

Audit Factory Capacity, MOQ, Lead Times, and ISO 9001 Quality Records

How to Find a Reliable Beauty Device Manufacturer in 2026?

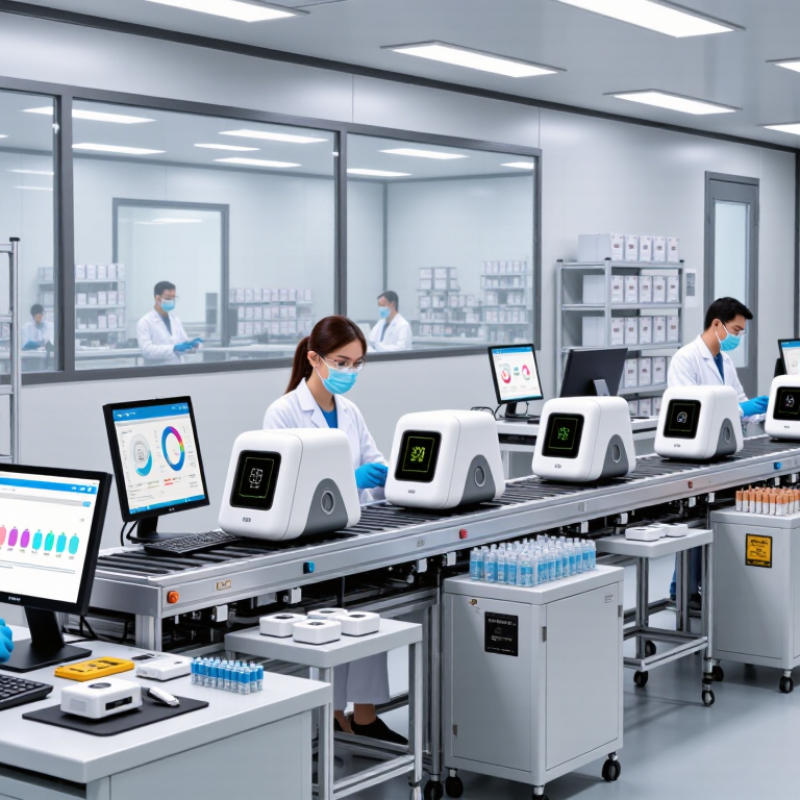
A factory audit should begin with real production evidence, not polished showroom samples. Ask to see active assembly lines, trained operators, testing equipment, and recent capacity records. Compare monthly output with your forecast and existing customer commitments. A factory may promise 50,000 units monthly, yet operate only one limited shift. Look for bottlenecks.

MOQ affects more than purchase price. Confirm whether the minimum applies per model, color, package, or customization. Request a written quotation showing tooling, packaging, spare parts, and inspection fees. A low MOQ can hide higher unit costs. I have seen attractive offers become expensive after packaging changes.

Lead times need evidence. Ask for production schedules from recent orders, including approval, assembly, testing, and shipment dates. Build extra time for design revisions and failed inspections. Delays happen. The important question is how the factory reports them and corrects the cause. Request ISO 9001 certificates, audit reports, corrective-action records, and sample quality logs. Check certificate validity and whether procedures match actual work. A document alone proves little. Review calibration labels, batch records, complaint trends, and final inspection results. If records look perfect, ask harder questions. Real factories usually show some recurring problems and explain how they reduced them.

How to Find a Reliable Beauty Device Manufacturer in 2026? - Audit Factory Capacity, MOQ, Lead Times, and ISO 9001 Quality Records
Audit Category Metric to Verify Practical Screening Benchmark Records or Evidence to Request Decision Signal
Factory Capacity Installed monthly production capacity Capacity should be at least 2 times the forecast monthly demand during the launch period. Production-line list, equipment register, staffing plan, monthly output records, and capacity calculation by model. Reject unsupported capacity claims that are not linked to equipment, labor, and shift data.
Factory Capacity Capacity utilization A utilization level of approximately 70%–85% generally leaves room for new orders, maintenance, and demand fluctuations. The latest 6–12 months of production plans, actual output, downtime logs, and overtime records. Very high utilization may create schedule risk; unusually low utilization requires an explanation.
Factory Capacity Critical-process ownership The manufacturer should identify which processes are performed internally and which are outsourced, especially assembly, firmware loading, optical testing, battery testing, and final inspection. Process-flow diagram, approved subcontractor list, supplier-control procedure, and incoming-inspection records. Uncontrolled outsourcing of safety-critical or performance-critical processes is a major risk.
MOQ Standard-product MOQ Obtain a written MOQ by model, color, packaging configuration, and certification variant; there is no universal MOQ for all beauty devices. Formal quotation showing unit MOQ, order value, packaging quantities, and any mixed-model rules. Use the lowest MOQ that matches your forecast without creating excessive component or packaging inventory.
MOQ Private-label or custom-tooling MOQ Separate the MOQ for existing tooling from the MOQ for new molds, custom electronics, firmware, or packaging. Tooling quotation, development agreement, sample approval plan, ownership terms, and tooling maintenance charges. Do not compare custom-development MOQ with ready-made product MOQ.
MOQ MOQ cost exposure Calculate the cash tied up in finished goods, components, printed packaging, and safety stock before placing the first order. Bill of materials, packaging purchase quantity, component lead times, payment schedule, and inventory assumptions. A low unit price is not attractive if the MOQ creates excessive slow-moving inventory.
Lead Time Sample lead time A standard sample is commonly planned at approximately 7–15 working days; custom samples require a separately agreed schedule. Sample order confirmation, engineering workload, prototype approval milestones, and sample inspection report. The quoted time should include engineering, procurement, assembly, testing, and shipment preparation.
Lead Time Mass-production lead time For a stable, approved product, a planning range of approximately 30–60 calendar days is often used; component availability can extend it. Capacity reservation, component lead-time matrix, production schedule, critical-path plan, and historical on-time delivery data. Require separate dates for deposit, component arrival, production completion, final inspection, and shipment readiness.
Lead Time On-time delivery performance Review at least 6 months of shipment history; an internal target of 95% or higher on-time delivery is a useful screening threshold. Order-level promised dates, actual shipment dates, delay reasons, corrective actions, and customer-approval records. Repeated delays caused by the same supplier or process indicate weak planning control.
ISO 9001 Certificate validity and scope The certificate should be current, issued by an accredited certification body, and cover the relevant design, manufacturing, assembly, or testing activities. Certificate number, issue and expiry dates, certification scope, site address, certification body, and verification result from the certification body. An ISO 9001 certificate alone does not prove product safety or regulatory approval.
ISO 9001 Document and change control Approved drawings, bills of materials, work instructions, software versions, and engineering changes should have revision status and approval history. Document-control procedure, engineering-change orders, revision logs, controlled work instructions, and obsolete-document records. Uncontrolled changes to components, firmware, or packaging can invalidate previous testing.
Quality Records Incoming inspection Critical incoming materials should have defined specifications, sampling rules, inspection results, and traceability to the supplier lot. Incoming-inspection reports, material certificates where applicable, supplier lot numbers, defect records, and quarantine logs. Materials used without recorded acceptance should be treated as a traceability gap.
Quality Records In-process and final inspection Inspection criteria should cover appearance, dimensions, electrical safety, charging performance, output function, labeling, and packaging as applicable to the device. Inspection standards, first-article reports, in-process check sheets, final inspection reports, and release authorization. Accept only records that identify product model, lot, date, inspector, measured result, and disposition.
Quality Records Calibration control Measuring equipment used for product acceptance should have an identifiable asset number, calibration status, due date, and traceable calibration record. Equipment register, calibration certificates, overdue-equipment review, and impact assessment for failed calibration. Expired or unidentified measuring equipment weakens the credibility of inspection results.
Quality Records Nonconformance and CAPA Each significant defect should have containment, root-cause analysis, corrective action, owner, due date, and effectiveness verification. Nonconformance reports, 8D or equivalent investigations, defect Pareto charts, CAPA closure records, and verification evidence. Repeated defects without verified corrective action indicate an ineffective quality system.
Traceability Batch and component traceability The factory should be able to link a finished-device lot to production date, operators, key components, inspection results, and shipment records. Serial-number or lot-number logic, ERP records, traveler sheets, component batch records, and mock-recall results. A traceability test should retrieve the requested records within one business day.
Product Compliance Safety and performance testing Testing should match the device technology and destination market, including electrical, battery, electromagnetic, optical, thermal, and biocompatibility considerations where applicable. Test plans, laboratory reports, risk analysis, technical file index, declarations, and product-specific certification records. Do not accept test reports for a different model, component configuration, or factory site without documented equivalence.
Final Audit Supplier scorecard Use weighted scoring: quality records 30%, capacity 20%, lead time 20%, compliance 15%, MOQ and commercial fit 15%. Completed audit checklist, objective evidence, open-action register, risk rating, and approval decision. Approve only when critical findings are closed or formally risk-accepted with deadlines.
Screening benchmarks are planning guidelines rather than universal industry requirements. Confirm the final specifications, testing, labeling, and regulatory obligations for the destination market and the specific beauty-device technology.

Verify Safety Claims Through FDA Databases, Clinical Data, and EMC Testing

How to Find a Reliable Beauty Device Manufacturer in 2026?

Safety claims should begin with searchable evidence, not attractive product photos. Check the FDA Establishment Registration and Device Listing databases, but remember that registration does not equal FDA approval. Search the FDA MAUDE database for adverse-event reports involving similar technologies. MAUDE contains millions of reports, although its records cannot prove that a device caused an injury. That limitation matters. A certificate alone is not enough.

Ask the manufacturer for peer-reviewed clinical data, study protocols, participant numbers, and follow-up periods. ClinicalTrials.gov listed more than 500,000 registered studies worldwide by 2024, showing how much research is publicly traceable. Small, unpublished tests deserve careful questions. Were controls used? Were skin types and treatment settings clearly reported? Claims based on ten participants may sound impressive, but they remain weak evidence.

EMC testing is another practical checkpoint. FDA electromagnetic compatibility guidance and IEC 60601-1-2 requirements address interference risks in applicable medical electrical equipment. Request the complete test report, including operating modes, cables, accessories, and failure limits. A device that passes in standby may behave differently during maximum output. This detail is often missed. Reliable suppliers should explain test conditions plainly, provide current reports, and accept independent verification. No report should be treated as permanent proof; design changes can invalidate old evidence.

Pilot-Order Samples Using ISO 2859-1 AQL Inspection Standards Before Scaling

How to Find a Reliable Beauty Device Manufacturer in 2026?

A factory tour can look impressive, but polished floors do not prove consistent quality. During pilot projects, I inspect sample orders using ISO 2859-1 AQL standards before discussing large production volumes. This method creates a measurable decision point. Define the lot size, inspection level, and acceptable quality limits before the devices arrive. Check charging, buttons, displays, housing seams, labels, and included accessories. Record every defect with photographs and batch numbers. A loose connector may seem minor, but repeated failures can damage customer trust.

Tips: Start with a small, controlled pilot order. Use an independent inspector when possible. Separate critical, major, and minor defects. Never let a supplier choose inspection rules after seeing the results. Ask for calibration records, material specifications, traceability documents, and corrective-action reports. Reliable manufacturers should explain failures without becoming defensive. They should also repeat inspections after corrections.

ISO 2859-1 AQL sampling does not replace technical testing or safety evaluation. It helps estimate lot quality through a consistent sampling plan. That distinction matters. My first supplier checklist was too broad, and it missed packaging damage during transport. Now I inspect cartons, seals, manuals, and device surfaces under realistic warehouse lighting. Compare pilot findings with the supplier’s own records. A manufacturer that hides defects is risky; one that investigates root causes may be worth further evaluation. No process is perfect. A careful review still beats an attractive promise.

ISO 2859-1 Pilot-Order Sampling Plan for Beauty Devices

General Inspection Level II, Normal Inspection, AQL 1.0%

Before scaling production, use a pilot order and inspect a statistically selected sample. The chart shows the ISO 2859-1 sample size for different lot sizes. At AQL 1.0%, the acceptance and rejection numbers are 3/4, 5/6, 7/8, 10/11, 14/15, and 21/22 respectively. These figures support consistent quality decisions without relying on company or brand data.

FAQS

How should a beauty device’s regulatory pathway be defined?

Start with the intended use, not factory photographs. Describe claims such as skin resurfacing or hair reduction precisely. Then record energy type, contact time, invasiveness, and target users. These details influence classification, testing, and launch timing. Wording changes everything.

What should manufacturers explain about market clearance?

Ask which regulatory pathway applies to the device. Some products may use an equivalence route, while others need stronger submissions. Do not accept vague phrases like “approved” without supporting details. Request the predicate comparison, submission records, and applicable exemptions. Verbal confidence is weak evidence.

How can European device classification be checked?

Request a written classification rationale before discussing certificates. Risk may depend on invasiveness, contact duration, active energy, and intended purpose. Software and intense light can create meaningful risks, even without skin penetration. Ask for the technical documentation index and clinical evaluation plan. A non-invasive appearance can mislead.

Which quality documents should a supplier provide?

Request the quality manual, device history records, calibration logs, and corrective-action reports. Confirm that the certificate matches the actual facility and product scope. Check its issuer and expiration independently. Production staff should explain inspections without reading a script. Watch the answer.

How should a factory audit compare samples and approved designs?

Compare the approved design with the physical sample in your hand. Check labels, instructions, calibration records, accessories, and software versions. Ask how failed units are isolated and traced by batch. Review change-control procedures for hardware, materials, and software. Small differences matter.

What clinical evidence supports safety and performance claims?

Ask for study protocols, participant numbers, control methods, skin types, settings, and follow-up periods. Raw results are more useful than polished summaries. A ten-person test may offer limited confidence. Small studies are not automatically useless. But question them.

How should safety databases and incident records be reviewed?

Search public registration and device-listing records for similar technologies. Review adverse-event reports, while remembering they may not prove causation. Ask whether complaints are tracked, investigated, and linked to corrective actions. Request incident-reporting responsibilities after launch. Records need context.

What should be checked in electromagnetic compatibility testing?

Request complete reports covering operating modes, cables, accessories, and failure limits. A device may behave differently at maximum output than in standby mode. Confirm the report matches the current design and production model. Independent verification can expose overlooked problems. Old evidence may expire.

Conclusion

Learning how to find a reliable beauty device manufacturer starts with regulatory clarity. Define the device category and intended use according to FDA 510(k) pathways and EU MDR requirements, then confirm that potential suppliers maintain appropriate ISO 13485 systems. Consider market demand and long-term growth forecasts, but prioritize documented compliance over promotional claims. A qualified manufacturer should also provide clear information about production capacity, minimum order quantities, lead times, equipment, and quality procedures.

Before making a large commitment, audit the facility and review ISO 9001 quality records, supplier controls, and corrective-action processes. Safety claims should be supported by searchable regulatory records, relevant clinical evidence, and electromagnetic compatibility testing where applicable. Finally, place a controlled pilot order and inspect samples using ISO 2859-1 AQL principles. This approach helps verify product consistency, packaging, documentation, and communication before scaling production, reducing avoidable risks while building a dependable long-term manufacturing relationship.

Aria

Aria

Aria is a dedicated marketing professional with a deep passion for innovative strategies and a keen understanding of our company's product offerings. With a wealth of experience in the industry, Aria excels at crafting engaging content that highlights the unique features and benefits of our......